Shakuntalam Impex infrastructure
MANUFACTURING INFRASTRUCTURE

Built for Precision. Ready for Scale.

Advanced processing, controlled environments, and export-ready handling built around the quality of natural ingredients.

UNIT 01

High-Vacuum Fractional Distillation Columns.

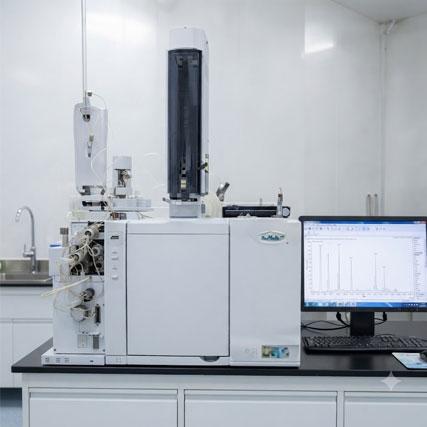
Our multi-stage fractional distillation columns operate under high vacuum to isolate volatile terpenes and aroma chemical fractions at controlled temperatures, preserving heat-sensitive natural molecules.

With computerized reflux control and temperature monitoring across every theoretical plate, we achieve sharp chemical cuts, separating Alpha Pinene, Beta Pinene, Limonene, and L-Menthone with up to 98%+ purity benchmarks.

High-VacuumLow Thermal Stress
Multi-ColumnHigh Throughput
SS-316LFood-Grade Purity
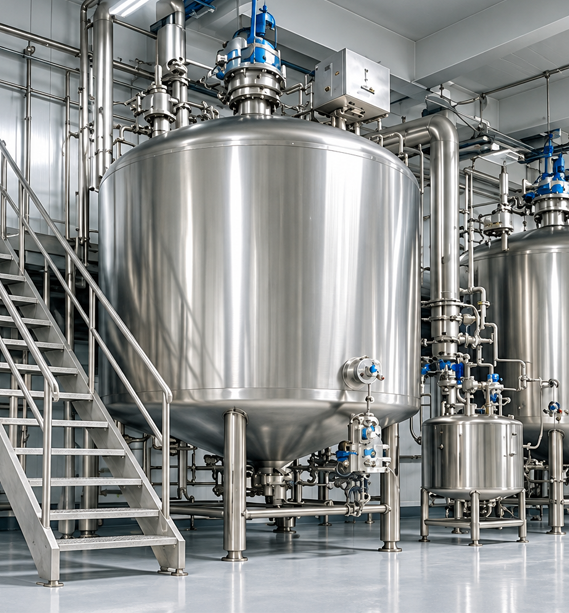
High-vacuum fractional distillation plant
UNIT 02

Controlled-Temperature Menthol Crystallization.

Producing pharmacopoeia-grade Menthol Bold Crystals requires slow, precision-monitored crystallization to achieve uniform, large hexagonal needle formation without entrained mother liquor.

Our computerized chiller circuits gradually lower temperatures in dedicated cleanrooms, followed by high-speed centrifugal drying to produce pristine, free-flowing L-Menthol crystals testing at a minimum 99.5% purity.

Min. 99.5%L-Menthol Assay
CleanroomControlled Air Flow
USP/BP/EPPharma Grade
Controlled-temperature menthol crystallization facility
UNIT 03

Nitrogen-Blanketed Bulk Tank Farm & Export Packing.

To prevent oxidative degradation of sensitive essential oils and terpene fractions, our bulk storage tank farm utilizes inert nitrogen gas blanketing.

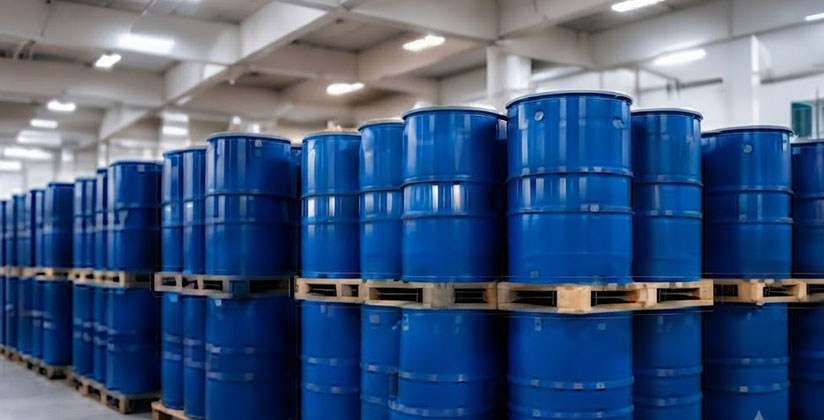
Our automated filling and packaging station operates in a dust-free environment, sealing products into epoxy-coated steel drums, fiber drums with food-grade LDPE liners, or IBC containers with tamper-evident export seals.

Stainless steel tank storage and export packing facility